Pipe and Tube Bending for Boilers
Waterwall, superheater and economiser tube bending, and helical coils wound in one piece.
What boiler work brings to a bending shop
Waterwall panels and tube bends, superheater and reheater elements, economiser coils, and the headers and downcomers around them.
Boiler work is where coiling and bending meet. A boiler is essentially a very large heat exchanger, so the parts that matter are long continuous runs of tube wound or bent to fit inside a fixed envelope. Coiling cold up through 10 inch pipe means a heavy economiser or heater coil can be made in one piece rather than welded together from segments, and every weld that does not exist is one that cannot fail in service.
Codes and standards: ASME Section I for power boilers and Section VIII for pressure vessels, both covered by the U and S stamps this shop holds. ASME B31.1 on the connected piping. Send your project specification with the enquiry and we will confirm in writing what we certify against before anything is cut.
Consistency from the first turn to the last
A coil that drifts in pitch will not fit the shell it was designed for, and finding that out at assembly is expensive. Consistent spacing from first turn to last is the number the process is set up to hold, so send the tolerance your drawing calls for rather than leaving it implied.
The shop has built eight multi-pass helical coils and a six multi-wound coil with as many outlets, and has worked in sizes that are not standard stock, including 7 inch and 9 inch pipe.
What to send with a boiler enquiry
Five numbers describe a bend: outside diameter, wall thickness, centerline radius, bend angle and the tangent length on each end. Add the material and the quantity and the job can be priced. A drawing, a sketch or a photograph of a marked-up print all work, and the quote form takes an attachment up to 25 MB.
For boiler work, a coil needs more description than a bend. Send the coil diameter, the pitch, the number of turns and passes, and where the inlets and outlets have to land. If the coil has to fit inside a shell, send that dimension too and say whether it is a hard limit.
Put the documentation requirements in the enquiry rather than in a later email. Material test reports, non-destructive testing and heat treatment all cost money and time. Retrofitting a documentation package onto a bend that has already been made is slow, and sometimes it is impossible.
Materials we bend
If the grade you need is not listed, ask. This is what comes through most often, not a limit.
What we can bend for you
How we would make it
Wall thickness, radius, material and schedule decide the process. Send the drawing and we will tell you which one fits.
Heat Induction Bending
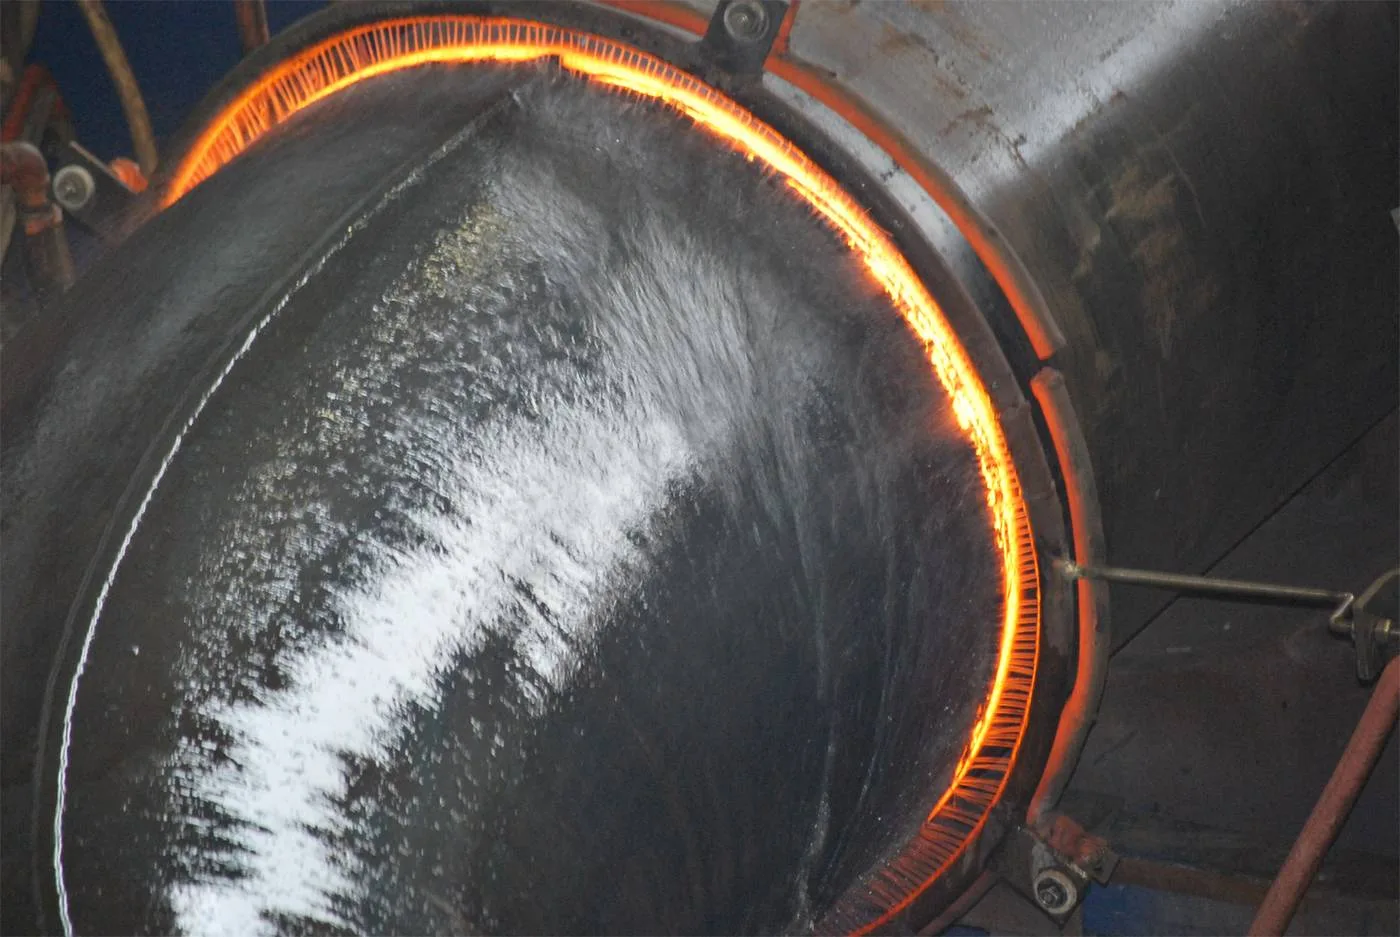
Cojafex induction bending up through 42″ O.D. and 4″ wall, in any radius, angle or plane.
Read moreCoiling
Helical, spiral wound and serpentine coils, cold, up through 10″ pipe.
Read moreCold Bending
Rotary draw bending on fourteen machines, with mandrels and wiper shoes where the radius needs them.
Read moreMandrel Bending
Ball mandrels and wiper shoes for tight radii and thin walls that would otherwise collapse.
Read moreLarge Diameter Pipe Bending
The work most shops turn away: up to 42 inch outside diameter and 4 inch wall.
Read moreStainless and Alloy Bending
Stainless, duplex, Hastelloy, titanium and nickel alloys, bent without wrecking the metallurgy.
Read moreQuestions we get from boiler buyers
Can you make boiler coils in one piece?
Coiling runs cold up through 10 inch pipe, which covers a lot of economiser and heater coil work in one piece rather than welded up from segments.
Do you hold the ASME S stamp?
Yes. The shop holds both the U and S stamps, covering Section VIII and Section I work.
Can you bend finned tube?
Yes. Finned tube is one of the sections the shop bends, along with round pipe and tube, channel, angle and wide flange.
Have a drawing? Send it over.
Send a drawing or a sketch and our team will get back to you with a quote.