Non-Destructive Testing
X-ray, ultrasonic, magnetic particle, liquid penetrant, PMI and hydro testing, to your specification.
Testing is set by your specification, not by us
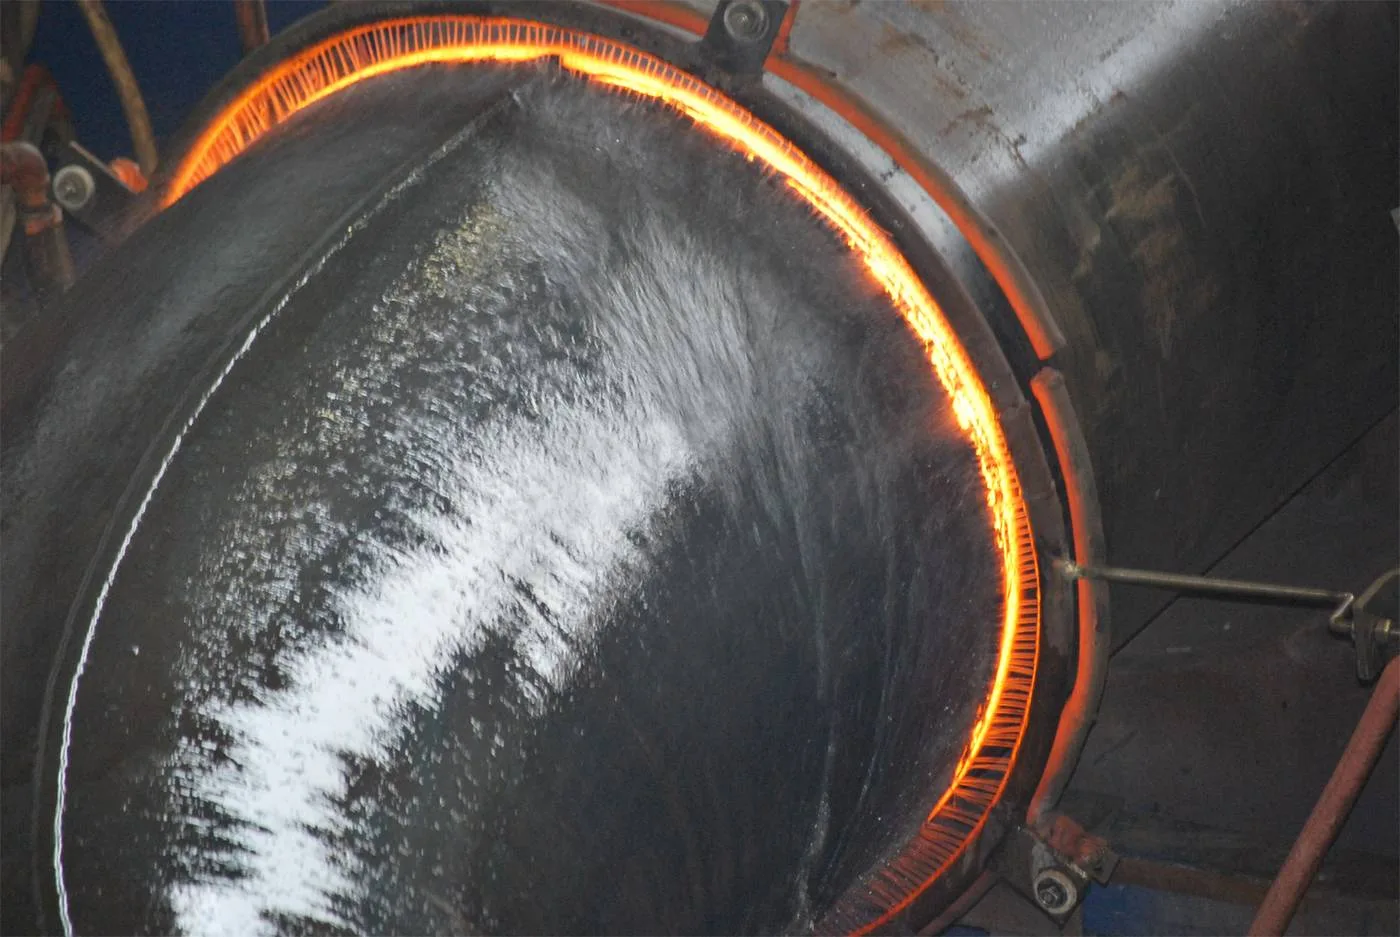
Every piece here is examined and cross-examined, and non-destructive testing is the part of that with a paper trail. According to your bending specification, American Pipe Bending can provide x-ray, heat treatment, stress relieving, liquid penetrant, Brinell hardness, Magnaflux, ultrasonic and magnetic particle testing, positive material identification, elemental analysis and hydrostatic testing.
Which of those apply is decided by your purchase order and the code the work is built to. We do not choose the regime. What we do is run as much of it as possible in house, because sending a bend out to be tested adds a transport leg, a handling risk and usually several days to a schedule that rarely has them spare.
The other reason to keep testing close to the bend is that a finding is cheap to act on while the part is still in the building. A rejectable indication found at the fabricator two states away is a different problem entirely.
Request a quoteWhat each test is looking for
Radiography and ultrasonic
Volumetric methods: they see inside the wall. Radiography images the whole thickness, ultrasonic measures it and finds planar defects. On a bend, ultrasonic wall thickness readings along the extrados are also how thinning gets verified against the specification limit.
Magnetic particle and liquid penetrant
Surface methods: they find cracks open to the surface. Magnetic particle works on ferromagnetic material, penetrant works on anything including stainless and non-ferrous. Both are quick, which is why they are usually the screening step.
Hardness, PMI and hydro
Brinell hardness checks that heat treatment did what it was supposed to. PMI and elemental analysis confirm the material is what the certificate says it is. Hydrostatic testing proves the part holds pressure.
Testing we can provide
Per your bending specification. Tell us the code and the acceptance criteria.
What to send, and what it costs to leave out
Five numbers describe a bend: outside diameter, wall thickness, centerline radius, bend angle and the tangent length on each end. Add the material, the quantity and the code and the job can be priced. The quote form takes a drawing up to 25 MB in PDF, DWG, DXF, JPG or PNG, and a photograph of a marked-up print is fine.
The things most often left out are the ones that change the price most. Documentation is the first: material test reports, non-destructive testing and heat treatment all have to be priced and scheduled from the start, and retrofitting a package onto a finished bend is slow and sometimes impossible. The delivery date is the second, because it decides whether the job is possible rather than what it costs.
The third is the acceptance criteria. Wall thinning on the outside of the arc and ovality through it are the two numbers a reviewer checks first. Tell us the limits and we will confirm the tightest radius that holds them before anything is cut. Finding the boundary at quote stage costs nothing; finding it at first article costs a length of pipe and a week.
Where a drawing calls out a bend that cannot be made as dimensioned, you will hear about it at quote stage rather than at delivery. That happens more often than it should, usually because an isometric was drawn without a bend schedule and the radius was never checked against the wall. Working back from an isometric to the five numbers each bend needs is routine here, and it normally catches at least one dimension that does not close.
Testing we can provide
Per your bending specification, not ours. Tell us the code and the acceptance criteria and we will say what runs here and what is subcontracted.
Other ways we bend
Wall thickness, radius, material and schedule decide the method. If you are not sure which fits, send the drawing and we will tell you.
Heat Induction Bending
Cojafex induction bending up through 42″ O.D. and 4″ wall, in any radius, angle or plane.
Read moreCoiling
Helical, spiral wound and serpentine coils, cold, up through 10″ pipe.
Read moreCold Bending
Rotary draw bending on fourteen machines, with mandrels and wiper shoes where the radius needs them.
Read moreMandrel Bending
Ball mandrels and wiper shoes for tight radii and thin walls that would otherwise collapse.
Read moreLarge Diameter Pipe Bending
The work most shops turn away: up to 42 inch outside diameter and 4 inch wall.
Read moreStainless and Alloy Bending
Stainless, duplex, Hastelloy, titanium and nickel alloys, bent without wrecking the metallurgy.
Read more
Have a drawing? Send it over.
Send a drawing or a sketch and our team will get back to you with a quote.